Your ERP Was Built to Record the Past. Here Is What Is Now Possible — and Why Most Manufacturing CEOs Do Not Know It Yet.
Only 43% of collected manufacturing data is used effectively, and 68% of ERP implementations are considered failures. The gap is not technology — it is design philosophy. Five gaps, a full comparison, and two paths for mid-market manufacturers depending on where their existing ERP stands today.
Conventional manufacturing ERPs were built for decision traceability — recording transactions so they can be audited. AI-enabled manufacturing ERPs are built for decision improvement — reconstructing reality in near real time and surfacing intelligence before decisions are made. Only 43% of collected manufacturing data is used effectively and 68% of ERP implementations are considered failures, because the design philosophy was never built for improvement. Five gaps explain the shortfall: design philosophy, production visibility, data entry lag, data silos, and causality. Two paths exist depending on whether the existing ERP is genuinely used or worked around.
Most manufacturing CEOs believe their ERP is working because data is going in. POs are raised. GRNs are logged. Inventory is tracked. Production orders are created. QC results are documented. The ERP has a record of everything that happened.
What it does not have — what it was never designed to have — is any understanding of what is happening right now, why it happened, or what should happen next. The ERP captures transactions. It produces no intelligence. And the gap between those two things is costing mid-market manufacturers more than most monthly management reviews will ever reveal.
This is not a criticism of the people who implemented the ERP. It is a description of what conventional ERPs were built to do. They emerged from an accounting and compliance mindset — the primary requirement was decision traceability, not decision improvement. Document the purchase order so it can be audited. Record the production entry so it can be traced. Capture the QC result so it can be reported. Every feature of a conventional ERP was designed to answer one question: what happened? Not: why did it happen, where is it happening right now, or what should we do about it?
Something has changed. AI has lowered the cost of building domain-specific software dramatically. For the first time, it is economically realistic to build a manufacturing intelligence system that starts from how manufacturing actually works — not from accounting logic. This blog explains the gap between what conventional ERPs deliver and what is now possible. And it explains why the answer depends on the current state of your existing system.
Direct answer: What is the difference between a conventional manufacturing ERP and an AI-enabled manufacturing ERP?
A conventional ERP is built for decision traceability — it records transactions (POs, GRNs, production entries, QC results) so they can be audited and reported. It answers: what happened? An AI-enabled manufacturing ERP is built for decision improvement — it reconstructs reality in near real time, connects siloed data sources, and surfaces intelligence before decisions need to be made. It answers: what is happening now, why did it happen, and what should we do about it? The production floor is no longer a black box. QC is no longer documentation after the defect. And the operating philosophies a manufacturer already believes in — Lean, Six Sigma, Theory of Constraints, export certification standards — are embedded as properties of the system, not bolted on through training.
Only 43% of collected manufacturing data is actually used effectively — leaving most ERP analytics potential untapped. 68% of ERP implementations are considered failures.
The two numbers belong together. Most manufacturing data that enters an ERP is never used to improve a decision. It is used to produce a report that describes what happened. The 68% failure rate is not primarily a technology failure — it is a design philosophy failure. ERPs were built to record. The expectation that recording would produce improvement was always the gap.
Source: Sigma Computing 2026 / Panorama Consulting 2025 via kreativecoretech
The Five Gaps That Explain Why Your ERP Is Not Delivering
GAP 01 — The Design Philosophy Gap: Traceability vs Decision Improvement
Conventional ERP: Built by technology companies with an accounting and compliance mindset. The primary design requirement: prove what decision was made. The ERP documents POs, GRNs, inventory positions, production entries. All backward-looking. All transaction-based. All designed to answer auditors, not operators.
AI-enabled ERP: Built from manufacturing operations logic. The primary design requirement: improve the next decision. Every data point captured is connected to a decision context — not just a record. The system asks: what does this data mean for what happens next on this floor, for this order, for this customer?
GAP 02 — The Production Black Box: Plan vs Reality
Conventional ERP: A production plan goes into the ERP. Reality happens on the floor. The ERP has no idea where a specific order is at this moment — how much is raw material, how much is WIP, how much is finished goods, whether the delivery will be on track. Nobody can tell from the system. They call the plant head.
AI-enabled ERP: Near real-time production visibility — where each order is in the process, what the current inventory state is across RM, WIP, and FG, whether delivery is on track or at risk. The floor is no longer a black box. It is a live system that the CEO can query.
From the field: In our engagements: "Where is order number X right now?" is a question that requires a phone call in most mid-market plants. An AI-enabled system answers it in seconds.
GAP 03 — The Data Entry Lag: Shift Notebooks to ERP
Conventional ERP: No mobile-based real-time data capture. The sequence: shift notebook by station. Excel file by supervisor. ERP entry by data entry staff the next morning. By the time the data reaches the ERP it is hours or days old — entered by someone who was not there when the event happened. The ERP is always behind reality.
AI-enabled ERP: Mobile-based capture at source. The operator or QC person records directly from the floor in real time — image capture, voice input, or guided forms. The data reaches the intelligence layer in seconds, not shifts. The person who made the observation is the person who records it.
From the field: We observed one company increase their data entry headcount from 7-8 to more than 25 after ERP implementation — because the system created more manual entry requirements than it eliminated. AI-based capture reverses this.
GAP 04 — The Silo Gap: Fragmented Reality, Human Consequences
Conventional ERP: ERP has purchase data. Tally has financials. Excel has the production plan. WhatsApp has real-time updates. Nobody has the bandwidth to pull from all four and construct what actually happened. People touch different parts of the same operation and report different realities. This creates human silos — accountability gets passed between functions because nobody has the complete picture. We have observed management meetings where three different functional heads presented three different versions of the same production week — each one correct from their data source, none of them the same reality.
AI-enabled ERP: Connected intelligence layer — one queryable reality assembled from all existing data sources, informed by the same data readiness that determines whether any AI initiative can succeed in the first place. The CEO asks a natural language question. The system draws from ERP, Tally, production records, and QC data simultaneously and returns a single coherent answer. Decision-making stops being a function of who you called last.
GAP 05 — The Causality Gap: Documentation vs Root Cause Intelligence
Conventional ERP: The ERP records that a rejection happened. Date, shift, quantity. The machine that produced it is in a different log. The material batch is in another system. The operator's observation is in a notebook. Root cause analysis requires a human to manually join all of these — which happens days later in a review meeting, long after the conditions that caused the defect have changed.
AI-enabled ERP: Contextual intelligence at the moment of the defect. Product spec, FMEA, control plan, machine manual, industry standards, live machine parameters, material batch data, operator knowledge, QC experience — all connected. The QC person gets a structured context for root cause analysis during production. Not documentation of the defect after the shift. Decision improvement while the machine is still running.
From the field: In aluminium die casting: a 4% reject rate against a 2% industry average costs approximately ₹15 lakhs per month in touch cost alone. The causality gap is where that money disappears.
73% of mid-market manufacturers are still in the AI pilot phase. Legacy integration is the top barrier for 55% of them — and 45% are still working from siloed data.
The pilot phase is not a technology failure. It is a design philosophy failure. Manufacturers who attempt to add AI to a conventional ERP discover that the ERP's data structure was never built to support the kind of connected, contextual intelligence AI requires. The solution is not more AI bolted onto an existing ERP. It is an intelligence layer built from the ground up on manufacturing operations logic.
Source: Kaufman Rossin / KORE1, State of Mid-Market ERP and AI Adoption, 2026
The Full Comparison — Conventional ERP vs AI-Enabled Manufacturing ERP
| Dimension | Conventional ERP | AI-Enabled Manufacturing ERP |
|---|---|---|
| Design philosophy | ✗ Built for transaction recording and audit trails | ✓ Built for decision improvement and reality reconstruction |
| Production visibility | ✗ Black box — plan recorded, reality unknown | ✓ Near real-time — where is each order, what is the current state |
| QC management | ✗ Documentation of defects after the fact | ✓ Root cause analysis during production using contextual intelligence |
| Data capture | ✗ Shift notebooks to Excel to ERP — hours or days of lag | ✓ Mobile-based capture at source — seconds, not shifts |
| Data silos | ✗ ERP + Tally + Excel + WhatsApp — structurally disconnected | ✓ Connected intelligence layer — one queryable reality |
| Lean / Six Sigma / TOC | ✗ Separate initiatives bolted on through training | ✓ Embedded as properties of the intelligence layer |
| Certification requirements | ✗ Manual documentation and audit preparation | ✓ Built into the system — compliance as a by-product of operation |
| Decision support | ✗ Reports generated after decisions are made | ✓ Intelligence surfaced before decisions need to be made |
| Customisation | ✗ Generalised logic — the plant bends to the ERP | ✓ Context-specific — the ERP is built for this plant's process |
| Mid-market affordability | ✗ Enterprise pricing for enterprise logic | ✓ Domain-specific AI has lowered the cost of custom intelligence |
What Is Now Possible — and Why
Three things have changed that make the AI-enabled manufacturing ERP economically viable for mid-market manufacturers today — when it was not five years ago.
Development cost has come down. AI has dramatically lowered the cost of building domain-specific software. Building a system that understands how aluminium die casting works, or how a textile buying house operates, or how a precision components plant manages its QC — this used to require enormous custom development budgets. Today, AI reduces that cost to a level where a mid-market manufacturer with ₹50-200 crore in revenue can access a system built for their specific context.
Domain expertise now drives the build. The intelligence of an AI-enabled ERP comes from the domain knowledge embedded in it — the product specs, the FMEA, the control plans, the lean principles, the Six Sigma tolerances, the Theory of Constraints logic, the ISO and IATF certification requirements. When the firm building the system understands manufacturing at this level — not just technology — the system can be contextually adapted for this plant, this product mix, this team.
Change management is manageable. The organisations that have made this transition successfully did so because the change management was designed alongside the technology — not as an afterthought. The system was built with the people who would use it, not delivered to them at go-live. That approach is now well-understood and repeatable.
The vision — what an AI-enabled manufacturing ERP integrates: Lean principles. Six Sigma tolerances. Theory of Constraints logic. ISO, IATF, and customer-specific export certification requirements. All embedded as properties of the intelligence layer — not separate training programmes bolted onto a generic system. The CEO's vision for how their plant should operate becomes the operating logic of the system. Contextually adapted for this plant, this product mix, this team's capabilities. Not a one-size-fits-all ERP that requires the plant to bend its operations into a shape the software understands.
The Two Paths — Which One Is Right Depends on Your Current ERP State
The answer is not always a new ERP. The right path depends on the current state of the existing system. Here is how to think about it:
Path 1 — New AI-Enabled ERP Built for Your Context
Right for: Companies where the existing ERP is poorly adopted, under-utilised, or fundamentally misaligned with how the operation works. The ERP was implemented but never became the real operating system. People work around it — notebooks, Excel, WhatsApp — because the ERP does not reflect how the plant actually operates.
Approach: Build a new manufacturing intelligence system starting from your process — not from accounting logic. Product master, FMEA, control plans, machine data, and operating standards are embedded from day one. Lean, Six Sigma, TOC, and certification requirements are properties of the system, not modules bolted on. The system is built with your team, in your context, for your specific manufacturing reality.
Outcome: A system your team actually uses — because it was built for how they work. Production visibility in near real time. QC intelligence during production. Procurement and inventory connected to demand. Decision-making that improves with every cycle.
Path 2 — AI Intelligence Layer Integrated With Existing Well-Running ERP
Right for: Companies where the core ERP is functioning — transactions, inventory, finance — but production planning and QC are the black boxes. The ERP is doing what it was designed to do. The gap is the intelligence it cannot provide.
Approach: Build a production planning intelligence layer and a QC root cause analysis layer that connects to the existing ERP via integration. The ERP stays for what it does well. The AI layer adds what it cannot do: real-time production visibility, causality-connected QC analysis, connected intelligence above the existing data. No rip-and-replace. No disruption to what is working.
Outcome: The production floor becomes visible. QC moves from documentation to decision improvement. The existing ERP investment is protected and extended — not discarded.
How to decide which path is right: One question: does your team currently use the ERP as their primary reference for production and QC decisions — or do they work around it? If they work around it — notebooks, WhatsApp, Excel are the real operating system — Path 1 is likely the right answer. If the ERP is genuinely embedded and the gap is intelligence above it — Path 2 is likely the right answer. The AI Advantage Diagnostic maps this clearly in one month.
AI-enhanced ERP implementations show 30-40% efficiency gains in facilities where the system is built for the operational context — not generically deployed.
The efficiency gain is not a function of AI capability. It is a function of fit. A system built for how this plant operates produces different results than a generic ERP with AI features added. The 30-40% gain appears consistently in implementations where the intelligence layer was built from domain understanding, not from technology first.
Source: top10erp.org, AI in ERP: The Next Wave of Intelligent ERP Systems, 2026
If your production floor is still a black box and your QC team is still documenting defects rather than preventing them — the gap has a cost. Let us map it. The AI Advantage Diagnostic tells you which path is right for your specific operation — and what the intelligence gap is costing you right now.
→ Enquire about the AI Advantage Diagnostic → stratai.io/contact
We assess your current ERP state, identify which path is right for your operation, and map the cost of the intelligence gap. We confirm availability within one business day.
Frequently Asked Questions
What is the main difference between a conventional ERP and an AI-enabled manufacturing ERP?
The core difference is design philosophy. Conventional ERPs were built for decision traceability — they record transactions (POs, GRNs, production entries, QC results) so they can be audited and reported. They answer: what happened? AI-enabled manufacturing ERPs are built for decision improvement — they reconstruct reality in near real time, connect data across siloed systems, and surface intelligence before decisions need to be made. They answer: what is happening now, why did it happen, and what should we do about it? Every feature difference between the two systems flows from this single difference in philosophy.
Does implementing an AI-enabled ERP mean replacing our existing system?
Not necessarily. The right answer depends on the current state of your existing ERP. If the ERP is poorly adopted — if your team works around it using notebooks, Excel, and WhatsApp as the real operating system — a new manufacturing intelligence system built for your specific context is likely the right path. If the ERP is functioning well for transactions but lacks production visibility and QC intelligence, an AI layer integrated with the existing system is likely the right path. The decision starts with an honest assessment of what the existing system is actually doing — not what it was supposed to do.
Why is production planning a black box in most conventional ERPs?
Conventional ERPs record the production plan — what was scheduled. They do not track the production reality — what is actually happening on the floor at this moment. There is no mechanism to capture where a specific order is in the process, how much material is at each stage, or whether the delivery will be on track, without a human physically checking and manually entering the information. By the time that information reaches the ERP it is hours old. An AI-enabled manufacturing ERP captures production state in near real time through mobile-based data capture and connected machine data — making the floor visible without manual reporting overhead.
How do Lean, Six Sigma, and ISO certification requirements fit into an AI-enabled ERP?
In a conventional ERP, Lean and Six Sigma are separate programmes — training initiatives, consultant engagements, improvement projects that run alongside the ERP without connecting to it. ISO and IATF certification requirements are managed through documentation systems that are separate from the production system. In an AI-enabled manufacturing ERP, these are properties of the intelligence layer — not bolt-ons. The system understands the control plan and flags deviations. It understands the FMEA and surfaces likely failure modes during QC. It understands the certification requirements and captures the evidence as a natural by-product of daily operations. Compliance becomes something the system does continuously — not something the team prepares for during audit season.
What is the realistic timeline for seeing results from an AI-enabled manufacturing ERP?
The timeline depends on which path is right for the operation. For the AI intelligence layer built above an existing well-running ERP — production visibility and QC intelligence improvements typically appear within Phase 1 of implementation as the connection layer is established and data starts flowing in real time. For a new manufacturing intelligence system built from the ground up — the diagnostic and build phase runs first, with P&L-visible impact typically appearing in Phase 2 as adoption establishes the system as the default operating reference. In both cases, the AI Advantage Diagnostic maps the realistic timeline for this specific operation before any commitment is made.
About StratAI
StratAI helps manufacturing firms in India build AI Advantage Systems. 10+ live deployments across textile, jewellery, furnishings, commodity processing, and component manufacturing. Official Registered Claude Partner and Anthropic Partner.
stratai.io/contact · palani@stratai.io · +91 99402 25924
"Your ERP was built to prove what happened. An AI-enabled manufacturing system is built to improve what happens next. The gap between those two sentences is the gap between where most mid-market manufacturers are and where they need to be."
— Palaniappan SN, Co-Founder, StratAI
What is the main difference between a conventional ERP and an AI-enabled manufacturing ERP?+
Does implementing an AI-enabled ERP mean replacing our existing system?+
Why is production planning a black box in most conventional ERPs?+
How do Lean, Six Sigma, and ISO certification requirements fit into an AI-enabled ERP?+
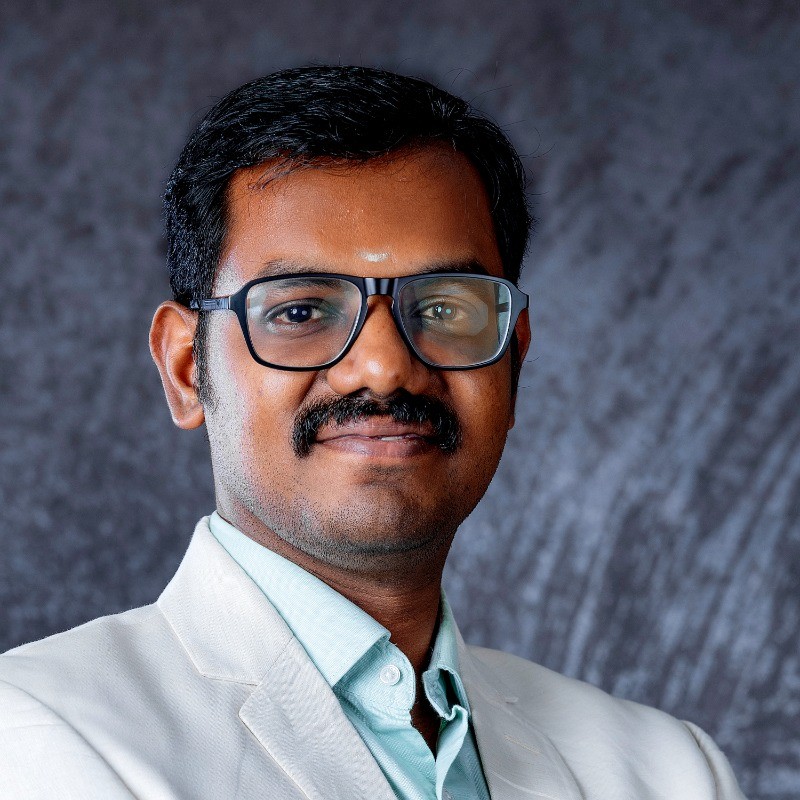
Palaniappan SN is a Business Strategy Consultant who has spent his career at the intersection of business strategy and operational reality — working across management levels from the boardroom to the shop floor to understand where organisations actually win and lose. His conviction is simple: AI should never be an experiment. It should be an advantage. That belief is the foundation of StratAI's AI Advantage Systems methodology — built not from technology-first thinking, but from the ground up, with the discipline to walk away from projects where the conditions for success don't exist.