AI in Manufacturing: Production Planning Reimagined with AI Starts Where the Spreadsheet Ends
AI in manufacturing: production planning reimagined with AI. How a job-by-process matrix and live context keep the plan alive, measured by weekly OTIF.
AI changes production planning by keeping the plan alive. This blog explains the job-by-process planning matrix, the progression from Context AI to Planning AI to simulation, Goldratt's Theory of Constraints applied to planning, the Depth, Swiftness, Completeness build method for mid-market plants, and why on-time-in-full delivery is the one metric to track every week.
Every plant head knows the call. A key customer's order will not ship on the date that was promised.
The plan said it would. The buffer said it would. The delay landed beyond both.
That is the tension this blog is about. Plants pad their plans with buffer time because production planning is uncertain. The delays that hurt most arrive beyond the padding. For a mid-market manufacturer, one strained relationship with a key customer can cost millions of dollars in lifetime value, far more than any buffer ever saved.
Large enterprises absorb this with planning systems, simulation tools and teams of expert planners. Mid-market plants have a spreadsheet, a production supervisor and experience. That gap is where AI in manufacturing earns its place.
This blog explains the planning problem, the logic of the fix and the method we use to build it. It is written as a design, because two of our engagements are only now beginning. Nothing here claims results we have not yet delivered.
Production Planning Is a Decision Made Under Shifting Context
In the plants we have studied, the production plan lives with one or two people, usually the production supervisor, and most others understand only their own part of it. The plan is a decision that must be remade every day, because the context under it keeps changing. Good planning is therefore a decision made with better information at the right moment, not a document.
Six events break a plan more often than any others.
| What happens | What it does to the plan |
|---|---|
| An urgent order arrives | Pushes out jobs that were already promised to other customers. |
| A machine breaks down | Removes capacity from a process the plan depends on. |
| Manpower falls short | Cuts capacity at the stations that need specific skills. |
| Material is unavailable | Blocks jobs that cannot start, and leaves machines waiting. |
| New orders land mid-week | Add rows to the plan that nobody has capacity for. |
| The customer slows down | Changes what was due when, and what can wait. |
No single planning approach fits every plant, because the right method depends on the business and the production system. Made-to-order and made-to-stock behave very differently. And the nature of the production system changes how hard the problem is.
| Production system | How hard planning is |
|---|---|
| Continuous flow | The easiest to plan. One route, steady rhythm. |
| Assembly line | Sits between the easiest and the hardest. |
| Batch production | The most complex. Many different jobs share the same processes in different sequences, so every change ripples through the plan. |
| Craft production | Easy again. Volumes are low and the work follows the skilled worker. |
The Buffer and the Gut Feel: How Plants Cope, and Where It Fails
Because the context keeps shifting, plants cushion for it. They add buffer time to quoted lead times. Then they run on gut feel, day-to-day priority and whatever pressure is loudest that day. This is a rational response to a hard problem. It is also a system with a known failure point.
The failure point is that delays happen beyond the buffer. When they do, the plant head and the CEO both feel it, because the cost lands on the customer relationship, not on a report.
Part of the reason the cycle repeats is that most plants do not learn from their own delivery record.
The cost of missing is not abstract in sectors that supply OEMs on tight terms. One logistics platform reports delay penalties of Rs 5,000 to Rs 50,000 per day per shipment for steel manufacturers supplying just-in-time customers (Fretron, predictive delivery glossary, accessed October 2026). Penalties are the visible cost. The strained relationship is the larger one.
The Planning Matrix: One Page That Shows the Whole Problem
Every production plan, however it is made, answers one question: what load does each customer job place on each process, and can each process carry it?
That question fits on a single page. List the customer job orders down the side. List the processes across the top. Mark the load each job places on each process. Then, for each process, add up the load and divide it by that process's capacity. The result is utilisation.
Figure 1: The production planning matrix. Jobs against processes, with utilisation calculated for each process.
The process with the highest utilisation is the candidate bottleneck. It is the point where the plan is most likely to fail, and where delays begin to spread to every job that passes through it.
An illustration, with numbers made up to show the logic and not drawn from any client. Suppose process P2 can carry 100 units a day. Three jobs place 30, 45 and 40 units on it. The total load is 115 units against a capacity of 100, so utilisation is 115 percent. On paper the plan is impossible, and a plant that finds this out on the shop floor finds out three days late.
The matrix is simple. Keeping it correct is the hard part. Every disruption in the earlier table changes it. A breakdown lowers the capacity of a process. An urgent order adds a row. A material delay blocks a cell. Recalculating all of this by hand takes hours, so people replan by phone and gut feel. The matrix goes stale, and the plan goes with it. Keeping it live depends on data that reaches decisions at the right moment. We call the layer that does this Context AI: a live model of jobs, processes, capacity and constraints that updates whenever anything changes.
Four families of constraint decide what a process can really carry. The planning AI has to know all four.
| Constraint | What the planning AI must keep current |
|---|---|
| Man | Skills, shifts, absence and who can run which process. |
| Material | What is available, what is expected, and which jobs are blocked until it arrives. |
| Machine | Real capacity, downtime and set-up time on each process. |
| Money | Overtime, expedite cost and the cash tied up in work-in-progress and stock. |
From Context AI to Planning AI to Simulation
Large enterprises solve this with planning software and expert planners. For a mid-market plant, the route that works is a progression, each stage built on the one before. Context AI holds the live picture. Planning AI plans against it. Simulation tests the plan before the plant commits to it.
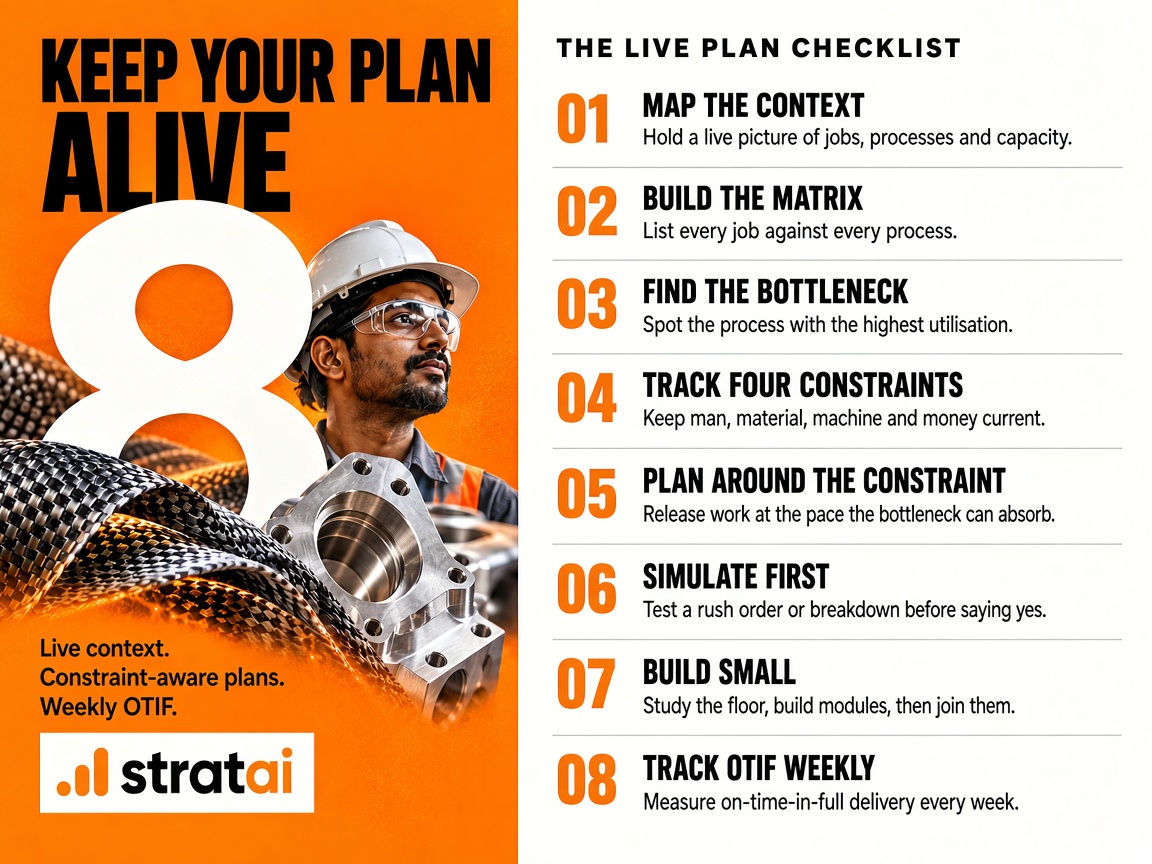
01 — Context AI: map the shifting context
The first job is to hold the live picture. Which jobs are open, which processes they need, what each process can carry today, and which constraints are active. This turns the matrix from a weekly spreadsheet into a living model that updates when something changes.
In practice: The planner sees the real load on each process today, not the load that was planned on Monday.
02 — Planning AI: plan against the constraints
Once the context is mapped, the planning AI is configured with the constraints across man, material, machine and money. It proposes a plan, shows utilisation for every process and flags the bottleneck. The planner still decides. The AI makes sure the decision starts from the full picture.
In practice: The planner sees which process will fail first, and why, before the shift starts.
03 — Simulation: test the disruption before committing
With a live model and a constraint-aware planner, simulation becomes possible. What happens to every promised date if a rush order is accepted? What happens if the key machine goes down for a day? The planner tests the answer before making the call.
In practice: The planner answers the customer from a simulation, not from a guess.
Why Throughput Rises Without New Machines: Goldratt's Theory of Constraints
The logic behind removing bottlenecks one at a time comes from Eliyahu Goldratt, who introduced the Theory of Constraints in his 1984 business novel The Goal, which its publisher, North River Press, describes as having sold more than 10 million copies (publisher description via Porchlight Books, accessed October 2026). Its central claim is simple. Every system has a constraint that limits its output. Improving anything other than that constraint does not raise the output of the whole system.
Goldratt formalised the approach as five focusing steps. The planning matrix and the planning AI map onto each of them.
| Focusing step | What it means | What the planning AI does |
|---|---|---|
| 1. Identify the constraint | Find the process that limits output. | Highest utilisation in the matrix, recalculated whenever context changes. |
| 2. Exploit it | Get the most out of the constraint as it is. | Never lets the bottleneck sit idle for want of material, people or a ready job. |
| 3. Subordinate everything else | Schedule all other processes around the constraint. | Releases work at the pace the bottleneck can absorb, so stock does not pile up. |
| 4. Elevate the constraint | Add capacity at the constraint if it still limits output. | Shows what extra capacity is worth, using real load, before money is spent. |
| 5. Repeat | The constraint moves. Start again. | Surfaces the next highest-utilisation process as soon as the first is lifted. |
This is how throughput rises from the same resources. The bottleneck is protected and fed. Everything else is planned around it. When it is lifted, the next constraint becomes visible, and the matrix shows which one it is.
The Build Method: Depth, Swiftness, Completeness
A planning system built from assumptions will be wrong. It will also take too long to find out. The method we use for mid-market plants is built around the opposite idea: learn on the ground, build small, and let the plant's own feedback shape the integrated system. It runs on a regular weekly cadence.
01 — Layer 1. Depth: study the process as it really runs
A detailed on-ground study of how production planning actually works today. Not the process as described in a meeting, the process as it runs on the floor. Then fix whatever can be fixed without any AI.
In practice: Many planning losses disappear at this stage because the process itself was never clear.
02 — Layer 2. Swiftness: build small, modular tools
Build ad hoc tools, each improving one key aspect of planning. Each one serves two purposes. It solves a real problem for the plant, and it produces feedback for the integrated system. A minimum viable version of one module is deployed, the gaps are found, and they are fixed.
In practice: The plant sees value in weeks, and every gap found becomes a requirement for the final system.
03 — Layer 3. Completeness: join the modules into one system
Once the modules have exposed what the plant really needs, build the integrated planning and simulation system in a modular way, with the context AI, the planning AI and the simulation joined into one working loop.
In practice: The integrated system is built from what has already been proven on the floor, not from imagination.
The principle is that today you no longer need to strive for perfection through endless assumption. You can build a minimum viable version of one module, deploy it, understand the gaps, fix them and build up. The same logic sits behind the first system we built for a furnishings client, where weeks of structured sessions with the founder extracted the tacit pricing logic that two people carried in their heads. The stitching sheet that followed went from one to one and a half hours to two seconds. You can read that story in what AI transformation actually looks like in practice.
In our experience, this is the right approach for mid-market firms. We do not believe it would work for enterprises, where scale, governance and procurement cycles call for a different path.
A planning system only helps if the team trusts it and uses it. That depends on the culture that makes the system get used, which is why the weekly cadence includes the planner and the supervisor from the first week.
The One Metric: On-Time-In-Full, Tracked Every Week
A planning system can be measured in many ways. We recommend one. Track on-time-in-full delivery every week, from the first week of the engagement, and let the trend tell the story.
The reason is simple. The buffer fails exactly where delivery fails. And a customer judges a plant on whether the order arrived on the promised date and in the promised quantity, not on how the plan looked.
Here is the baseline from one of our two starting engagements. In our engagement baseline, a jewellery manufacturer currently delivers orders in an average of 15 days, against a customer expectation of 7. Our planned trajectory is below. Please read it as a plan, not as a result.
| Stage | What is done | Average delivery time |
|---|---|---|
| Baseline | Observed at the start of the engagement. | 15 days, against 7 expected |
| Phase 1 | Detailed on-ground study of planning, and fixes that need no AI. | Target: about 12 days |
| Phase 2 | Small modular tools, each solving one planning problem. | Target: about 9 days |
| Phase 3 | Integrated AI planning with dynamic context and simulation. | Target: under 7 days, with about 5 as the goal |
Figure 2: Planned trajectory of average delivery time. Targets, not delivered results.
These numbers are targets. The engagement is beginning, and we will not claim an outcome before it exists. What we commit to is the discipline: measure on-time-in-full every week and review the movement with the plant head. The trend, not the forecast, tells us what is working.
Two Engagements Beginning, and What We Will Do First
We are about to start production planning AI projects with two very different businesses: a jewellery manufacturer, and a service provider that cuts wire to customer specification for the aerospace industry.
The two plants run different production systems, which is the reason the planning AI cannot be a copy of one design. In both, the first step is the same. Study how planning really runs today, on the ground, and fix what can be fixed without AI. Then build small, deploy, learn and join the modules into one system.
This is not a project that finishes in two or three months. It takes about a year to build properly. Early modules deliver value along the way, and the integrated system arrives once the plant has shown us what it needs. Done carefully, the benefit compounds.
What to Do on Monday Morning
You do not need AI to start learning from your own plan. Four steps cost nothing but a morning.
| Step | Action |
|---|---|
| 1 | Draw the planning matrix for your ten most important open jobs. Jobs down the side, processes across the top. |
| 2 | Mark the load each job places on each process, and write down each process's real daily capacity. |
| 3 | Calculate utilisation for every process. Note which one is highest. That is your first candidate bottleneck. |
| 4 | For every order that ships this week, record the promised date and the actual date. Start your own on-time-in-full record. |
Most plants discover, within one exercise, that the plan loads some process beyond what it can carry. That discovery is the beginning of better planning, with or without AI.
If the matrix shows a process loaded beyond what it can carry, a short study is the fastest way to find out why, and what to build first. Every week the plan stays in a spreadsheet is another week in which a disruption can land beyond the buffer.
Frequently Asked Questions
What is production planning with AI in manufacturing?
Production planning with AI keeps the plan connected to the live shop floor. It maps the shifting context of man, material, machine and money, loads every job against every process, finds the bottleneck and proposes a plan against real constraints. The planner can then simulate a rush order or a breakdown before committing. The planner remains the decision maker. The AI makes sure each decision starts from the full picture instead of a spreadsheet that was correct only on Monday morning.
Why does Excel production planning break down in mid-market plants?
Excel holds orders, capacity and material but not the live shop floor. It is correct when it is made and stale after the first urgent order, breakdown, manpower gap or material delay. Recalculating it by hand takes hours, so teams replan by phone and rely on buffer time and gut feel. It also usually sits with one or two people, so the plan stalls when they are unavailable. The failure is not the tool. It is that context changes faster than a spreadsheet can follow.
What is OTIF and why should a plant track it every week?
OTIF means on-time-in-full. A delivery counts only when it arrives on the agreed date and in the full ordered quantity. A plant should track it weekly because it is the measure the customer feels and the place where buffers fail. Fretron reports that most Indian manufacturers do not measure it accurately, often rebuilding it afterwards from delivery challans. Tracked weekly from the first week of an engagement, it shows whether each planning change is working.
How does the Theory of Constraints apply to AI production planning?
Goldratt's Theory of Constraints says every system has a constraint that limits its output, and improving anything else does not raise throughput. In planning, the constraint is the process with the highest utilisation in the job-by-process matrix. AI recalculates it as context changes, schedules other processes around it, shows what extra capacity at the constraint is worth, and surfaces the next constraint once the first is lifted. That is how throughput rises from the same resources.
How long does it take to build an AI production planning system for a mid-market plant?
It is not a two or three month project. Building it properly takes about a year. The work starts with a detailed on-ground study and fixes that need no AI, moves to small modular tools that each solve a real problem, and ends with an integrated planning and simulation system. Early modules deliver value along the way, and a weekly cadence keeps the build tied to what the plant actually experiences.
Does AI replace the production planner?
No. Planning is a decision made under shifting context, and the planner owns that decision. AI gives the planner a live model of load and capacity, flags the bottleneck and lets them test a disruption before acting. It takes over the recalculation that today happens by hand and by phone. The planner's experience matters more, not less, because it is now applied to a plan that is based on the full picture.
About StratAI
StratAI helps mid-market manufacturing firms in India build AI Advantage Systems that show up in the P&L, not just in dashboards. We work as an embedded partner, not a project vendor. Official Registered Claude Partner and Anthropic Partner.
stratai.io/contact | palani@stratai.io | +91 99402 25924
"A production plan is not a spreadsheet. It is a decision, remade every day under shifting context. AI in manufacturing gives that decision the context the spreadsheet never had. And the only honest way to know it is working is to track on-time-in-full delivery, every single week."
What is production planning with AI in manufacturing?+
Why does Excel production planning break down in mid-market plants?+
What is OTIF and why should a plant track it every week?+
How does the Theory of Constraints apply to AI production planning?+
How long does it take to build an AI production planning system for a mid-market plant?+
Does AI replace the production planner?+
Palaniappan SN is a Business Strategy Consultant who has spent his career at the intersection of business strategy and operational reality — working across management levels from the boardroom to the shop floor to understand where organisations actually win and lose. His conviction is simple: AI should never be an experiment. It should be an advantage. That belief is the foundation of StratAI's AI Advantage Systems methodology — built not from technology-first thinking, but from the ground up, with the discipline to walk away from projects where the conditions for success don't exist.